Our projects, part by part

Eight parts actually machined in our workshop, with the material, machine, tolerance and lead time. Our customers' names and drawings never leave the workshop: the exact dimensions of each part are provided on request, in line with our confidentiality agreements.

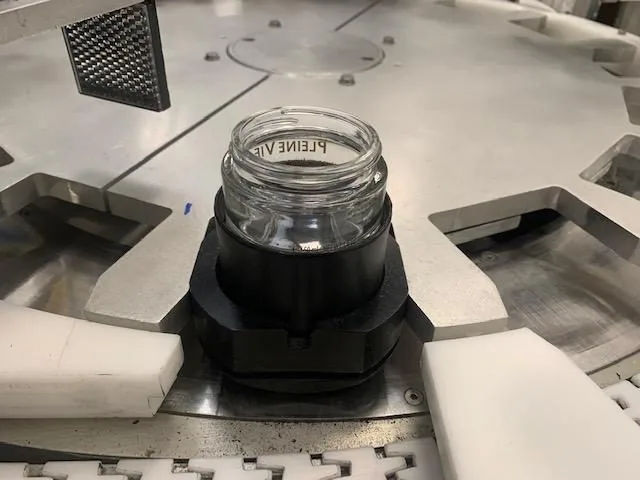
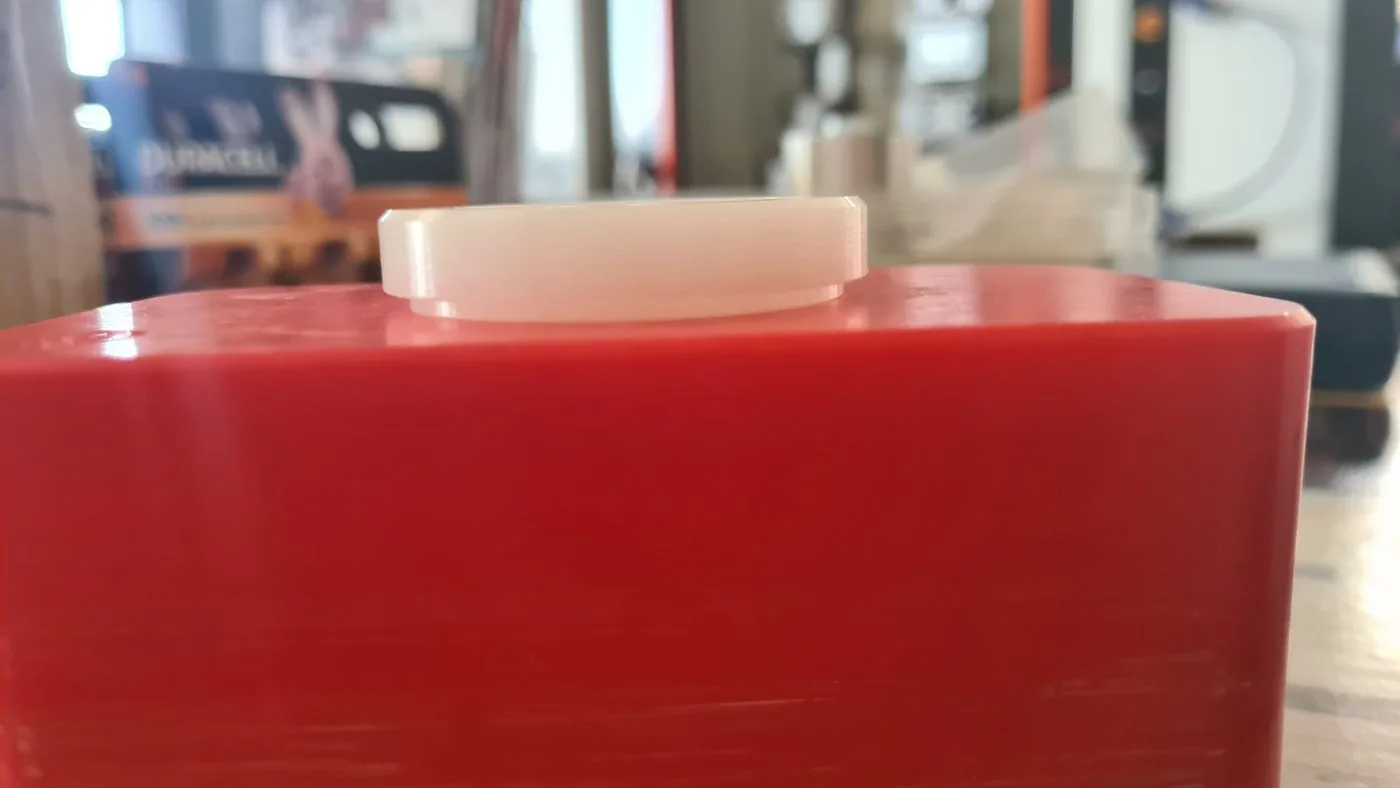
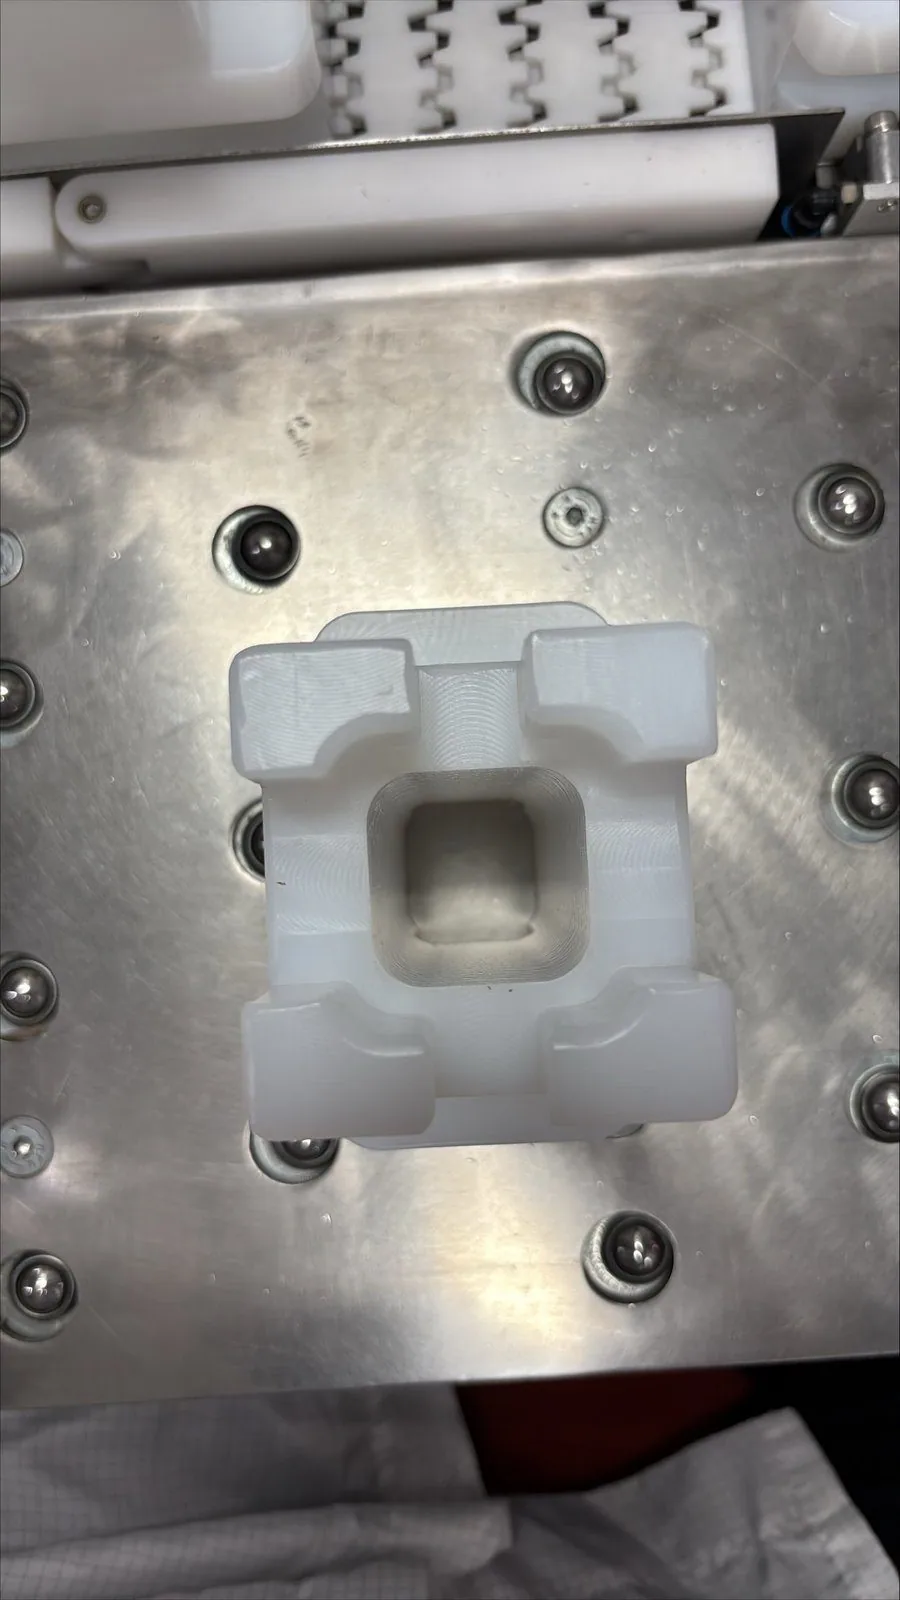
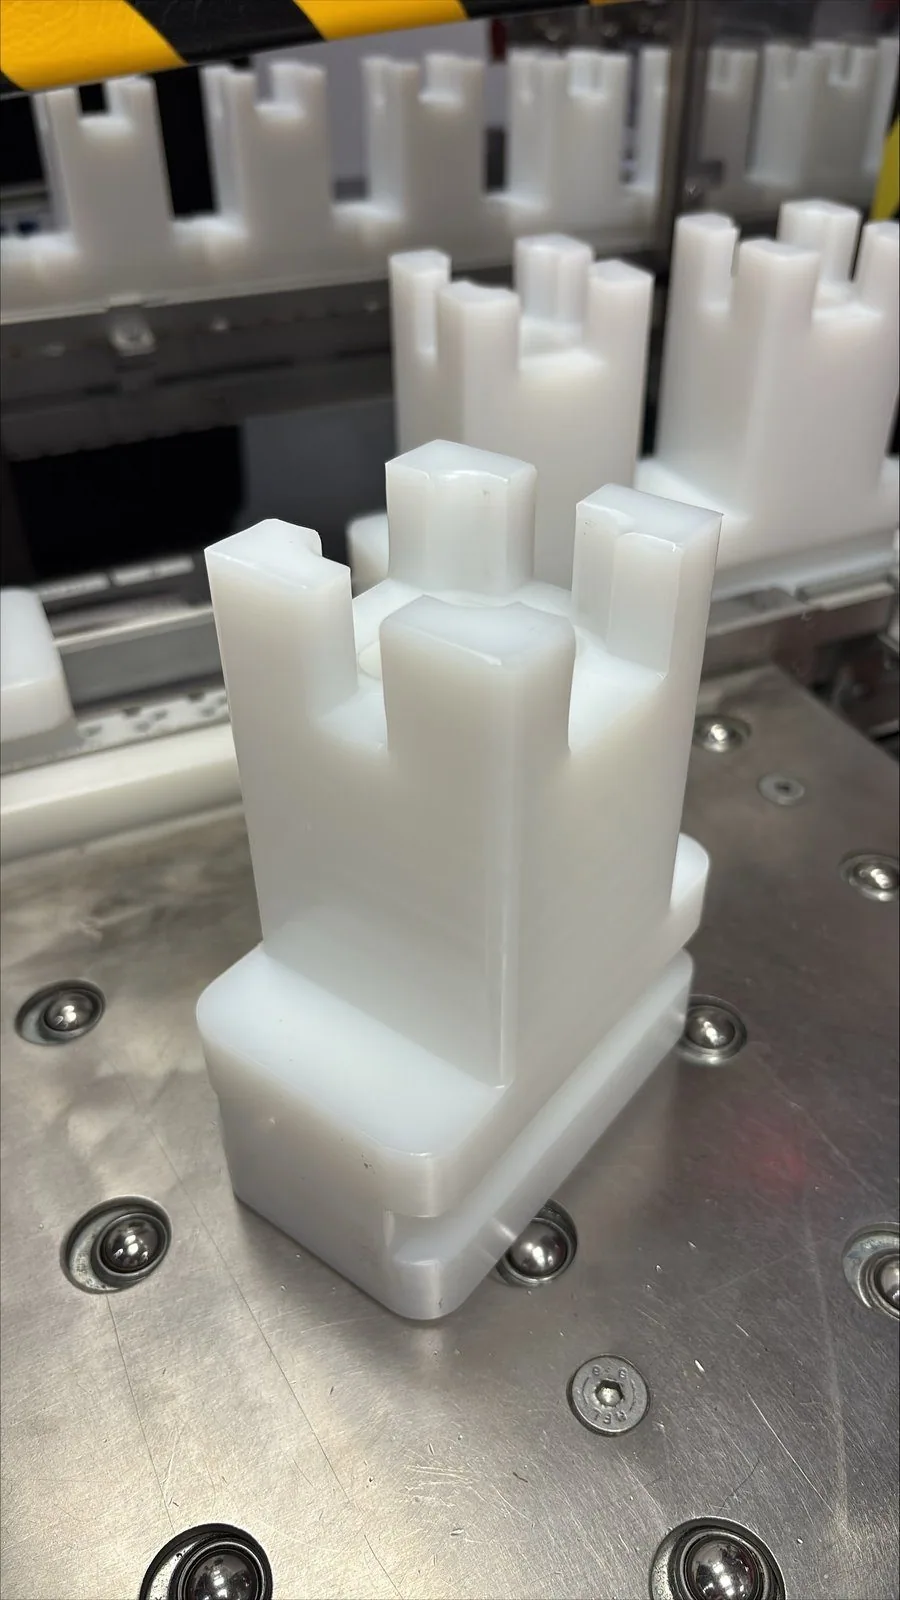
Custom-machined HDPE puck for a perfume bottle, mounted on the line — Alésage XC HDPE gripper fingers machined from solid, mounted on the line — Alésage XC
Luxury / Perfume

Custom packaging puck for a perfume bottle

Produced in three formats from a single design, each puck matches the shape of its bottle to hold it on the packaging line.

MaterialPEHD 500
Machines3-axis CNC machining centre and SBC milling machine
OperationsMilling of the cavity to the bottle profile, drilling, deburring
ToleranceFunctional fit on the bottle profile — ISO 2768
Quantity150 parts, 3 formats
Lead time3 weeks
Inspection3D dimensional inspection of the internal shape (KEYENCE XM-5000)
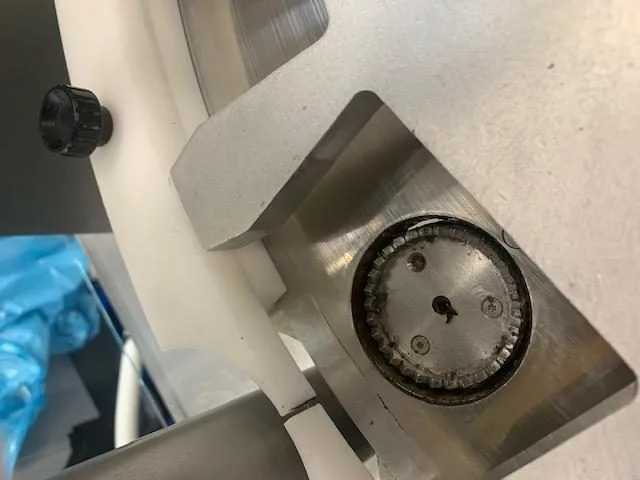
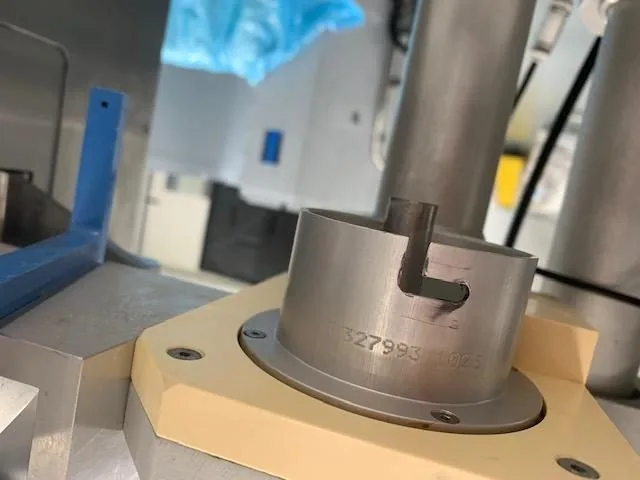
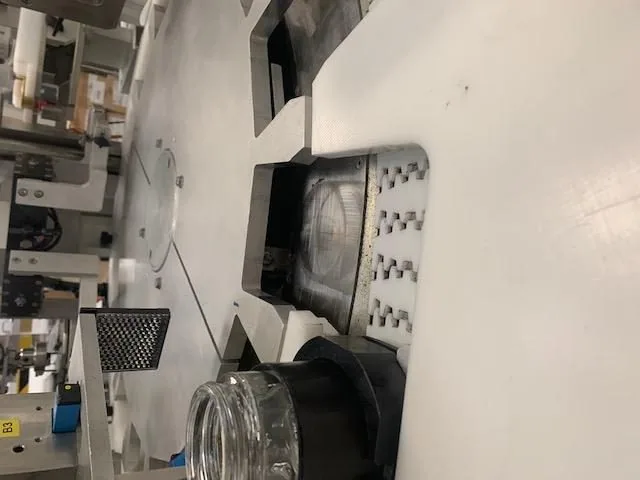
Anodised aluminium star wheel and orienting unit — Alésage XC Detail of the fluted holding fixture that receives the bottle, machined on a MAZAK centre — Alésage XC Turned stainless steel orienting unit part, mounted on its adjustment holder — Alésage XC Overall view of the orienting station on the line — Alésage XC
Cosmetics / Special-purpose machine

Star wheel and orienting unit for a packaging line

Set of machined and assembled parts forming a gripping and turnover module for an automated packaging line.

MaterialMachined and anodised aluminium
MachinesMAZAK machining centres
OperationsMilling, drilling, tapping, mechanical assembly
ToleranceISO 2768
Quantity1 star wheel and 50 pucks
Lead time3 weeks
InspectionDimensional inspection of parts before assembly
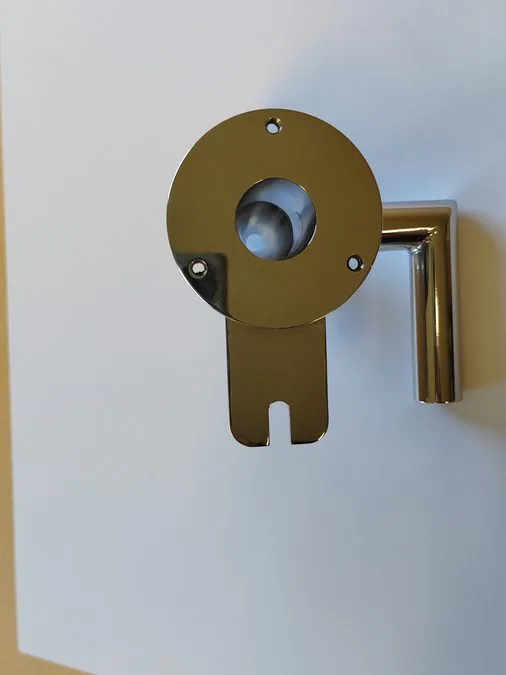
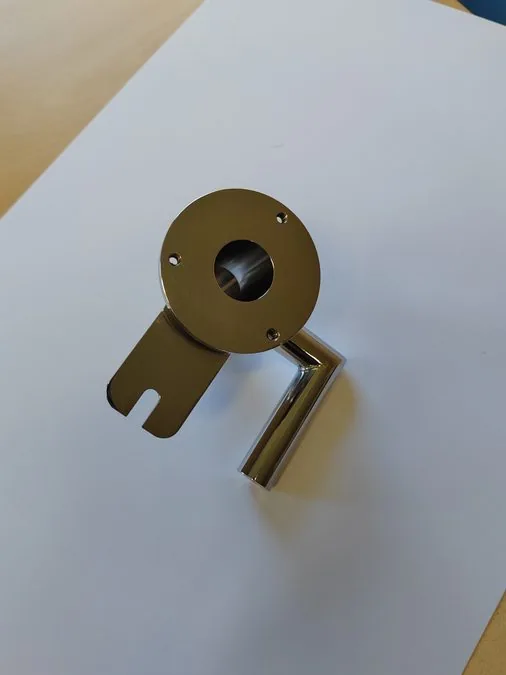
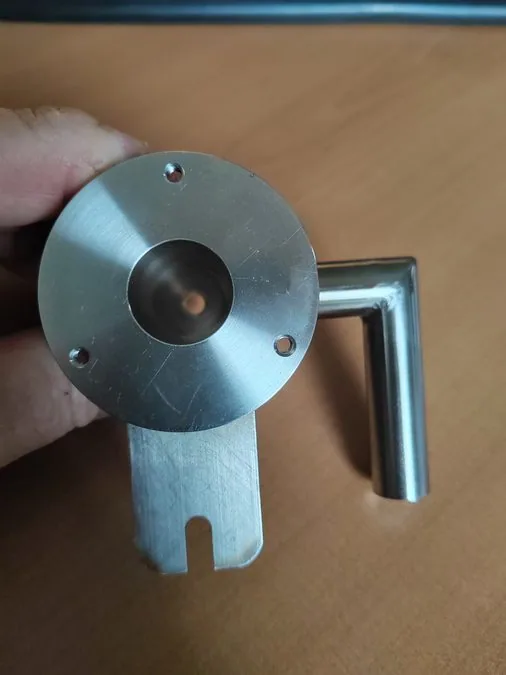
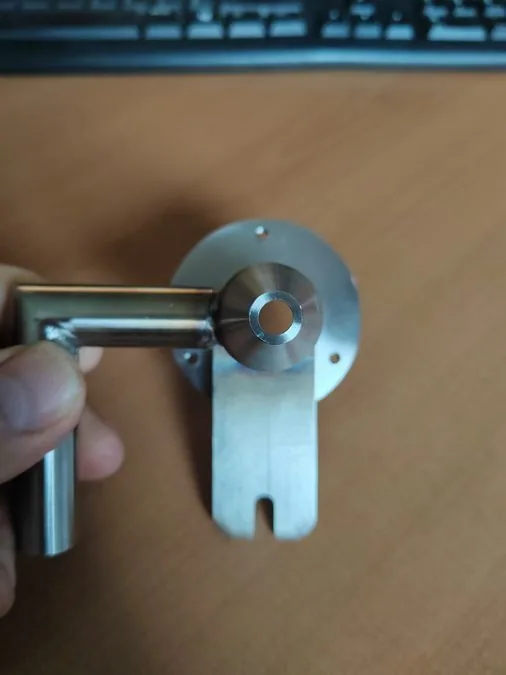
Medical injection nozzle in 316L stainless steel, centring flange and mounting bracket — Alésage XC Medical injection nozzle, three-quarter view — Alésage XC Detail of the centring flange and the mirror-polished bore — Alésage XC Medical injection nozzle held in the hand, part to scale — Alésage XC
Medical · Class IIb device

Medical injection nozzle with mounting bracket

The tapered bore, the part's main function, guides the injection flow and seals it. The IT7 tolerance was achieved directly by CNC turning, with no rework or grinding. Mirror polishing was entrusted to a specialist partner: Ra 0.8 µm required, Ra 0.2 µm achieved. Each part was delivered with its metrology report.

Material316L stainless steel, EN 10204 3.1 certificate, traceable heat number
MachinesMAZAK QT20N CNC lathe and MAZAK HCN 5000 horizontal machining centre
OperationsExternal and internal turning, taper boring, Ø 3 mm through-hole drilling, flange milling
ToleranceIT7 — ±0.009 mm on the bore; flange flatness 0.05 mm
Surface finishRa 0.2 µm after mirror polishing
Quantity12 parts, pilot run
Lead time8 working days, polishing included
InspectionKEYENCE XM-5000 part by part, report supplied with delivery, batch traceability
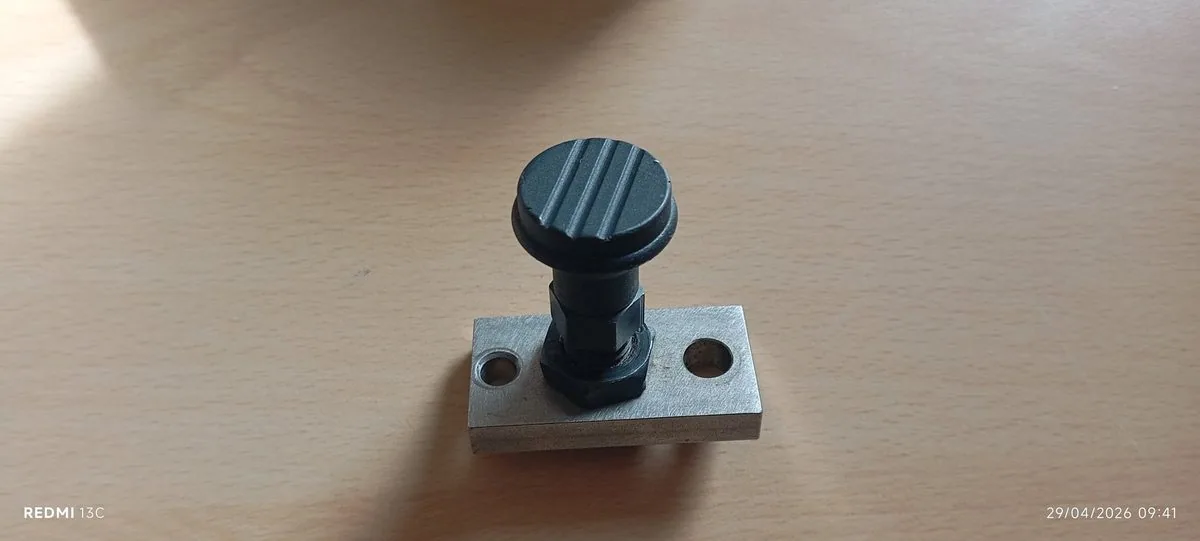
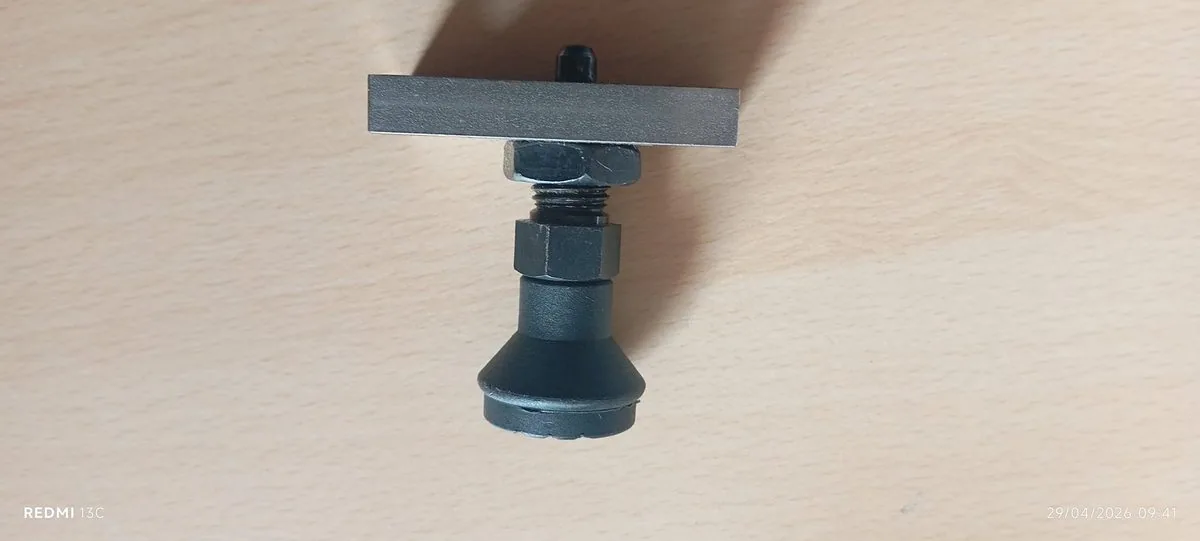
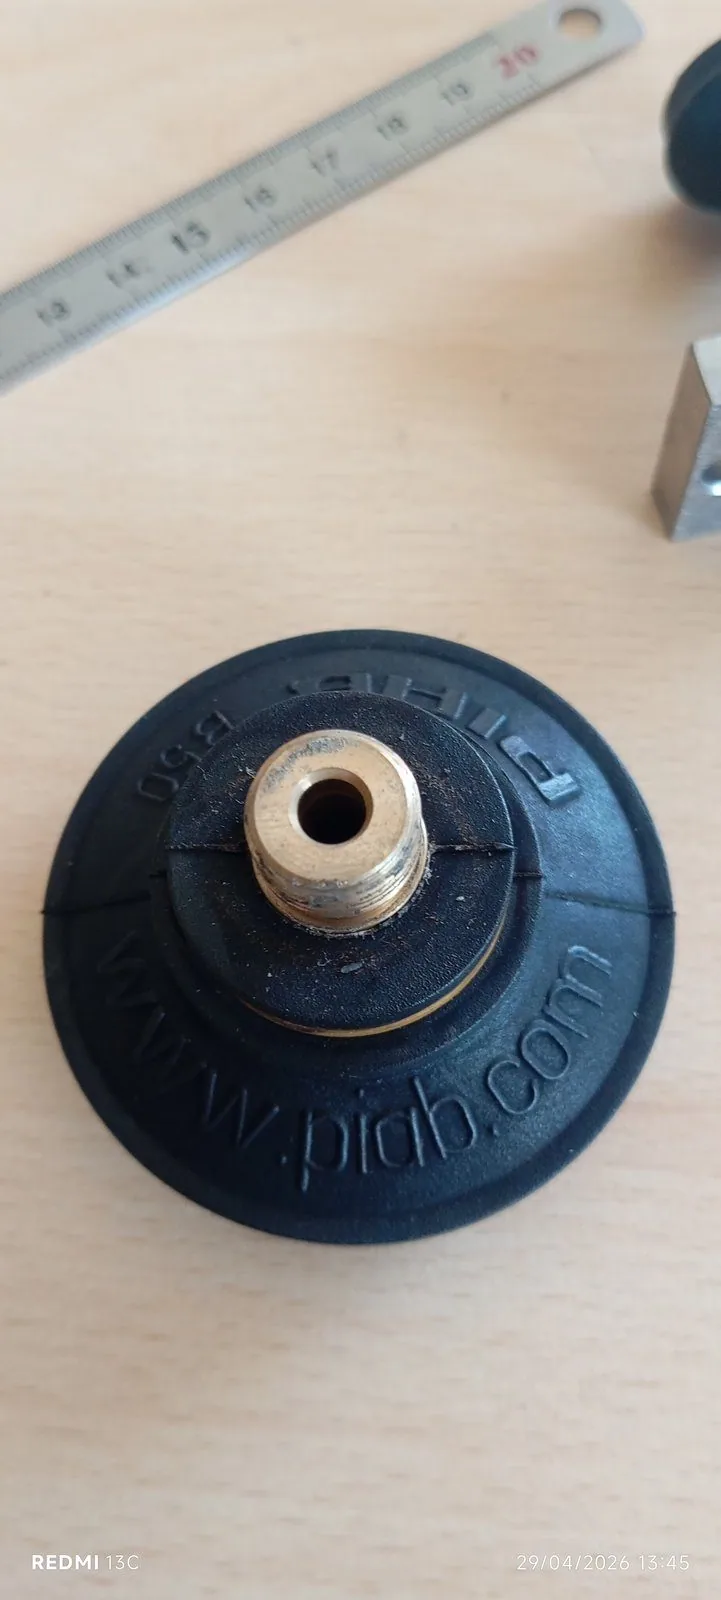
Knurled locking finger on stainless steel base — Alésage XC Suction cup mounted on its rod and mounting plate — Alésage XC Suction cup seen from above with its machined brass tip — Alésage XC
Luxury / Perfume

Cartoner tooling — locking finger and suction cup

Contribution to building a cartoner for perfume bottles, with many items in different materials. Shown here: the locking finger and the gripping suction cup.

MaterialMirror-polished stainless steel, aluminium, polycarbonate
MachinesMAZAK HCN 5000 machining centre and DUFOUR 131 conventional milling machine
OperationsMilling, drilling, mirror polishing, assembly
ToleranceISO 2768-mK
Lead time3 to 4 weeks for the whole set
InspectionDimensional survey on the customer's sample before manufacture
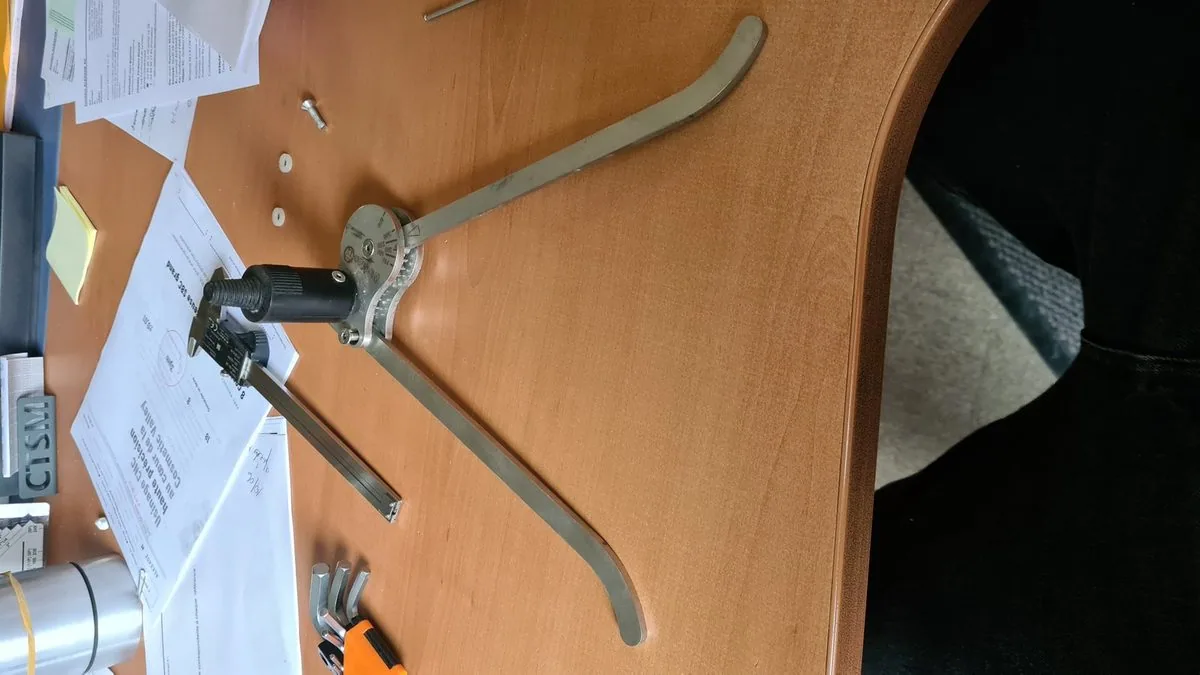
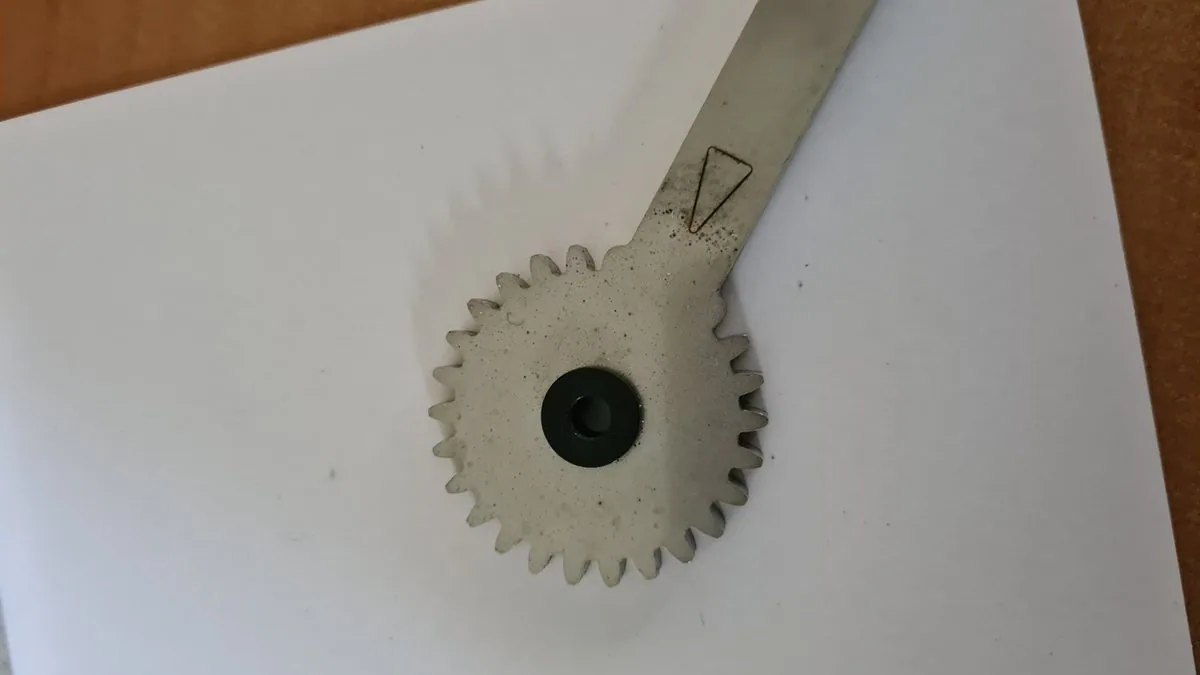
Stainless steel diameter inspection callipers, articulated curved arms — Alésage XC Toothed sector of the compass, laser cut then finish-machined — Alésage XC
Sanitation

Diameter inspection callipers

Set of small parts laser-cut and then machined, for the assembly of an inspection compass.

MaterialStainless steel
MachinesLaser cutting and MAZAK QT20N CNC lathe
OperationsLaser cutting, turning, deburring
Tolerance±0.1 mm
Quantity10 parts
Lead time2 to 3 weeks, cutting included
Dosing valve block reassembled after the valve plugs were reproduced — Alésage XC Checking the fit of a plug in its valve body — Alésage XC Detail of a reproduced plug and its seal — Alésage XC
Cosmetics / Process

Valve plug — reverse engineering and reproduction

The wear part was removed and measured at the customer's site, then reproduced new and identical. The plug was made in three parts to make fitting the seals easier.

MaterialTreated stainless steel
MachinesMAZAK SQT 200 MSY CNC lathe
OperationsDimensional survey of the wear part, reproduction turning, fitting
ToleranceSealing fit
Quantity16 parts
Lead time4 weeks, treatment included
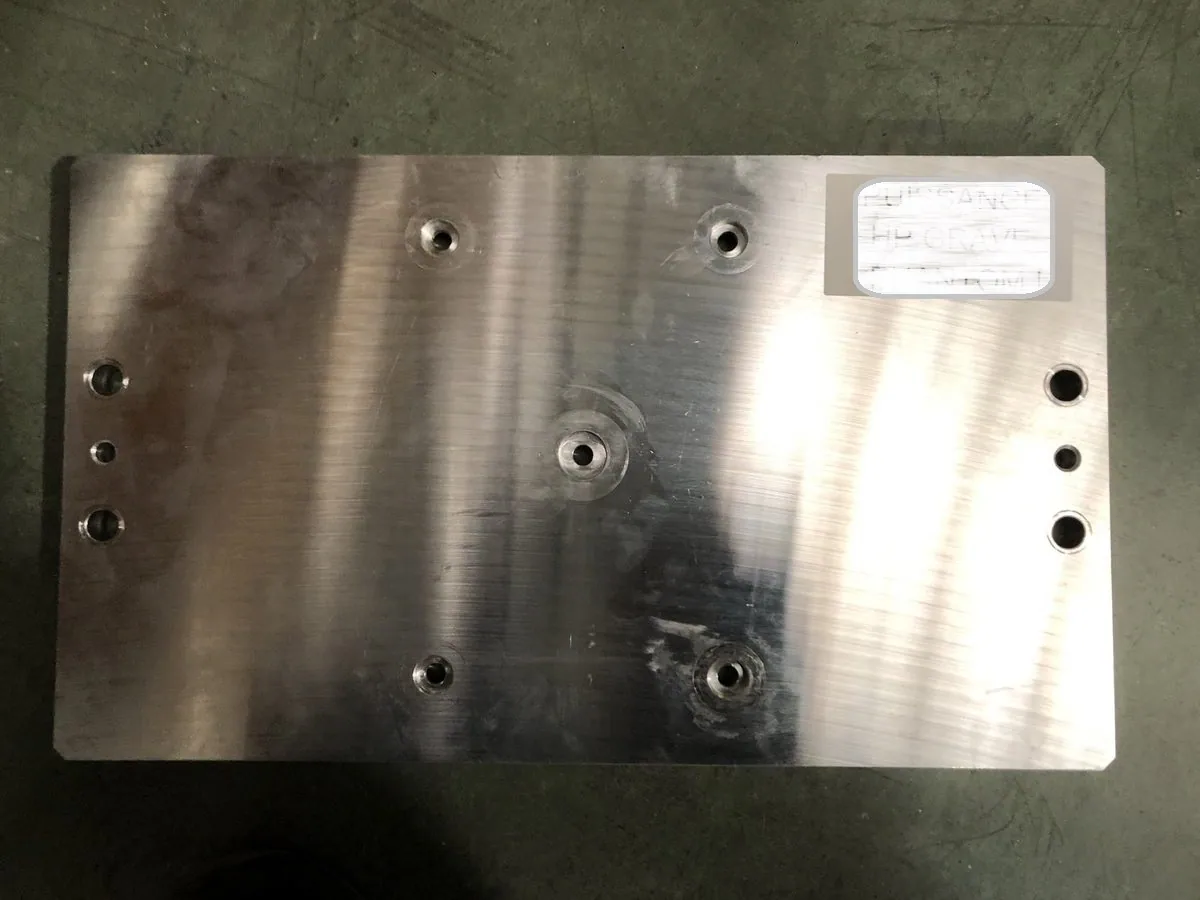
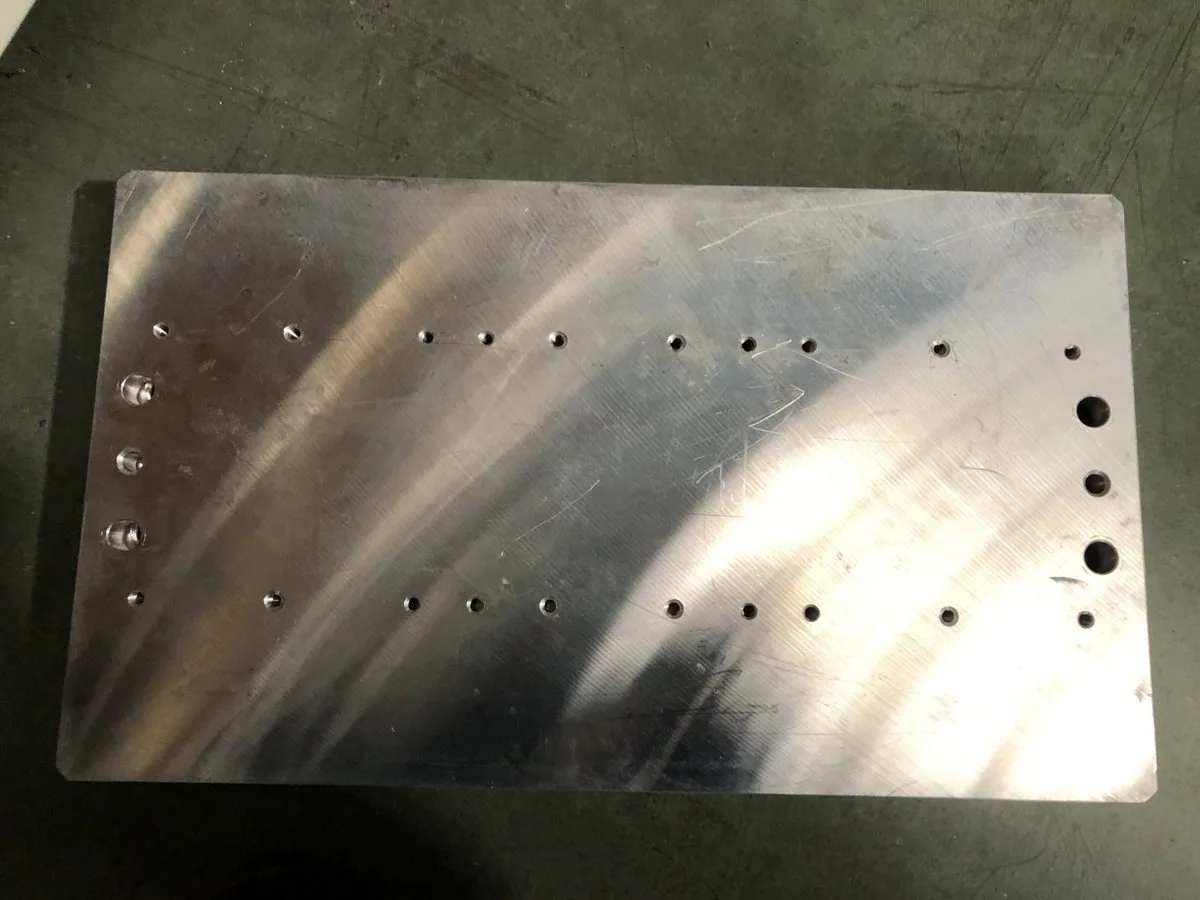
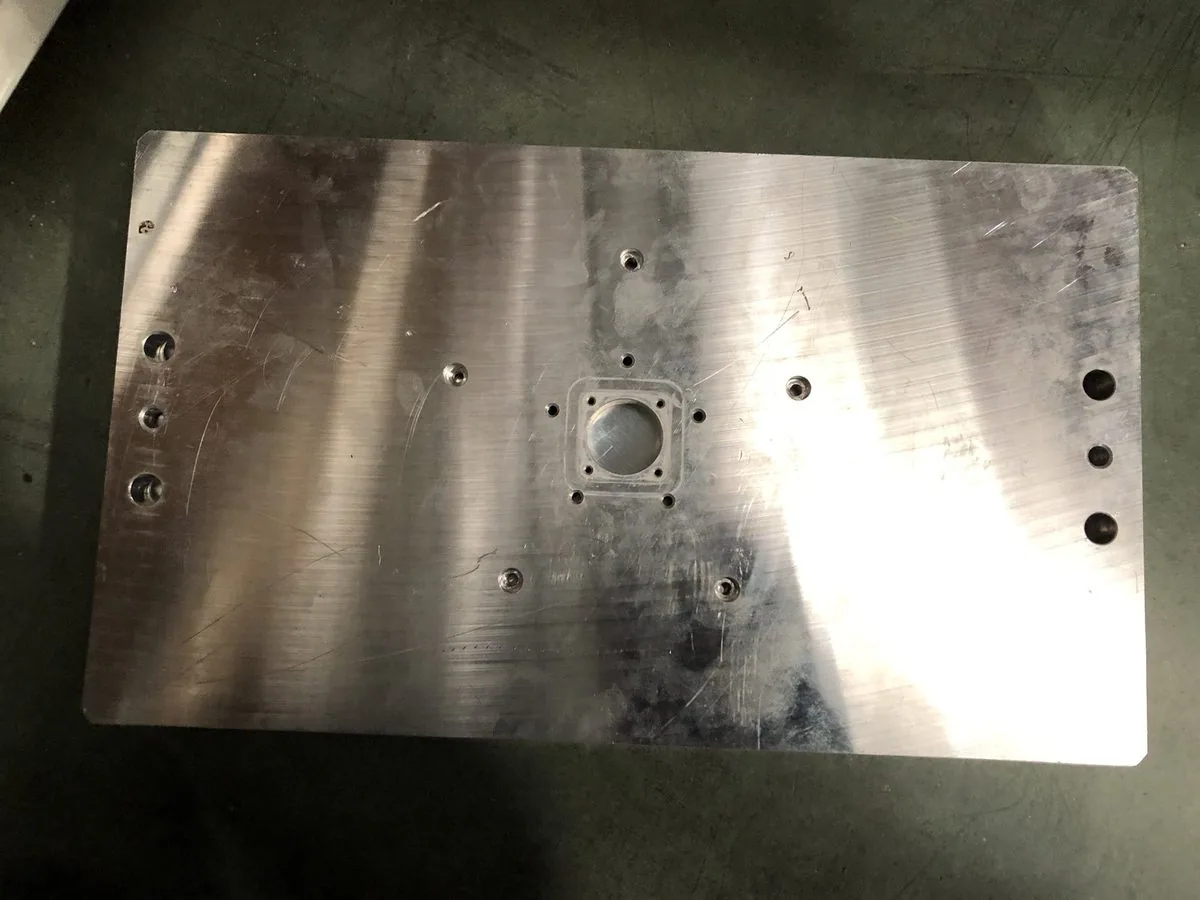
Machined aluminium holding fixture plate, locating holes — Alésage XC Holding fixture plate, overview — Alésage XC Detail of the central cavity and holes — Alésage XC
High-fidelity audio

Holding fixture base plate

One-off part made before the launch of series production: central cavity, row of locating holes and counterbores.

MaterialAluminium
MachinesMAZAK HCN 4000 horizontal machining centre
OperationsMilling of the cavity, locating holes, counterbores
ToleranceTo drawing
Quantity1 part
Lead time2 weeks
Machined removable insert for cosmetic filling tooling — Alésage XC
Perfume & Cosmetics

Removable insert for filling tooling

Filling tooling insert designed to be removed easily: servicing and cleaning are done in production, without dismantling the whole station.

MachiningMulti-operation
DesignRemovable, easier maintenance

A part similar to one of these projects? Send your drawing or a photo: quote within 24 hours, or 48 hours when we supply the material.

Request a quote → Change parts Special-purpose machines
📞 Call Request a call back Request a quote