Precision boring and honing: fits that have to hold
Bearing seats, bushes, guides, sealing bores: these are the dimensions that make a machine work. We hold them by direct machining and, when the fit requires it, by honing.
- IT5–IT6 routinely on functional diameters, without external grinding.
- Ra ≤ 0.4 µm depending on geometry, down to Ra 0.2 µm on a polished bore.
- Quote within 24 hours, or 48 hours when we supply the material.
What we hold
- IT5–IT6 routinely on functional diameters: threaded rings, sealing surfaces, sliding fits.
- IT7, ±0.009 mm on the tapered bore of a medical nozzle, achieved by CNC turning with no rework or grinding.
- Ra ≤ 0.4 µm depending on geometry, down to Ra 0.2 µm on a polished bore.
Equipment
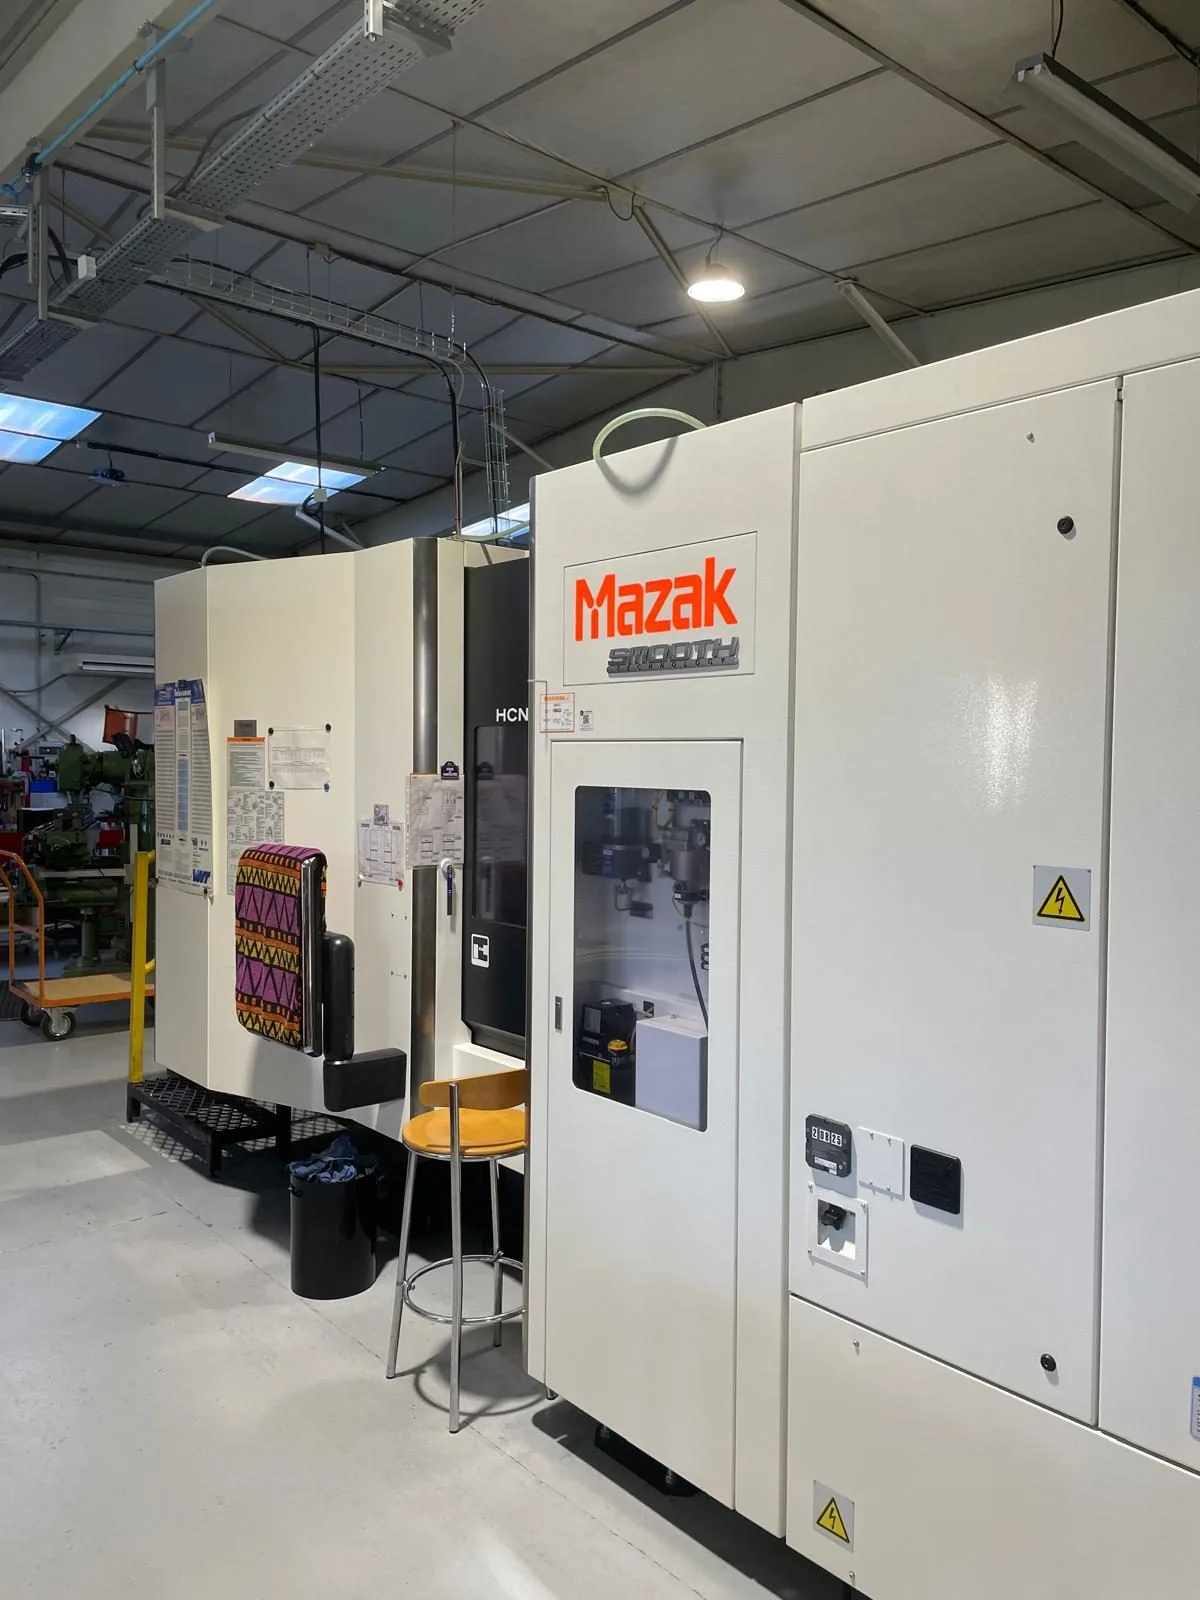
- MAZAK HCN 5000 (two), HCN 4000 and H400 horizontal centres: 4-axis machining, bores on several faces without unclamping.
- MAZAK CNC lathes, including the SQT 200 MSY for turn-milling in a single clamping.
- SUNNEN honing machine: bore honing for tight fits (bearing seats, bushes, guides, plain bearings).
- Inspection: KEYENCE XM-5000, Deltronic DH400 profile projector, inspection report on request, and standard gauges (internal micrometers, plug gauges).
Direct machining or honing?
Most functional bores come out to size directly from our MAZAK machining centres and lathes: this is how we routinely hold IT5–IT6 without external grinding.
SUNNEN honing comes in when the fit is tight and the geometry of the bore matters as much as its diameter: bearing seats, bushes, guides, plain bearings. We tell you at the quote stage which route we will take.
A tight bore to hold? State the tolerance in your request: quote within 24 hours, or 48 hours when we supply the material.
Send my drawing ↓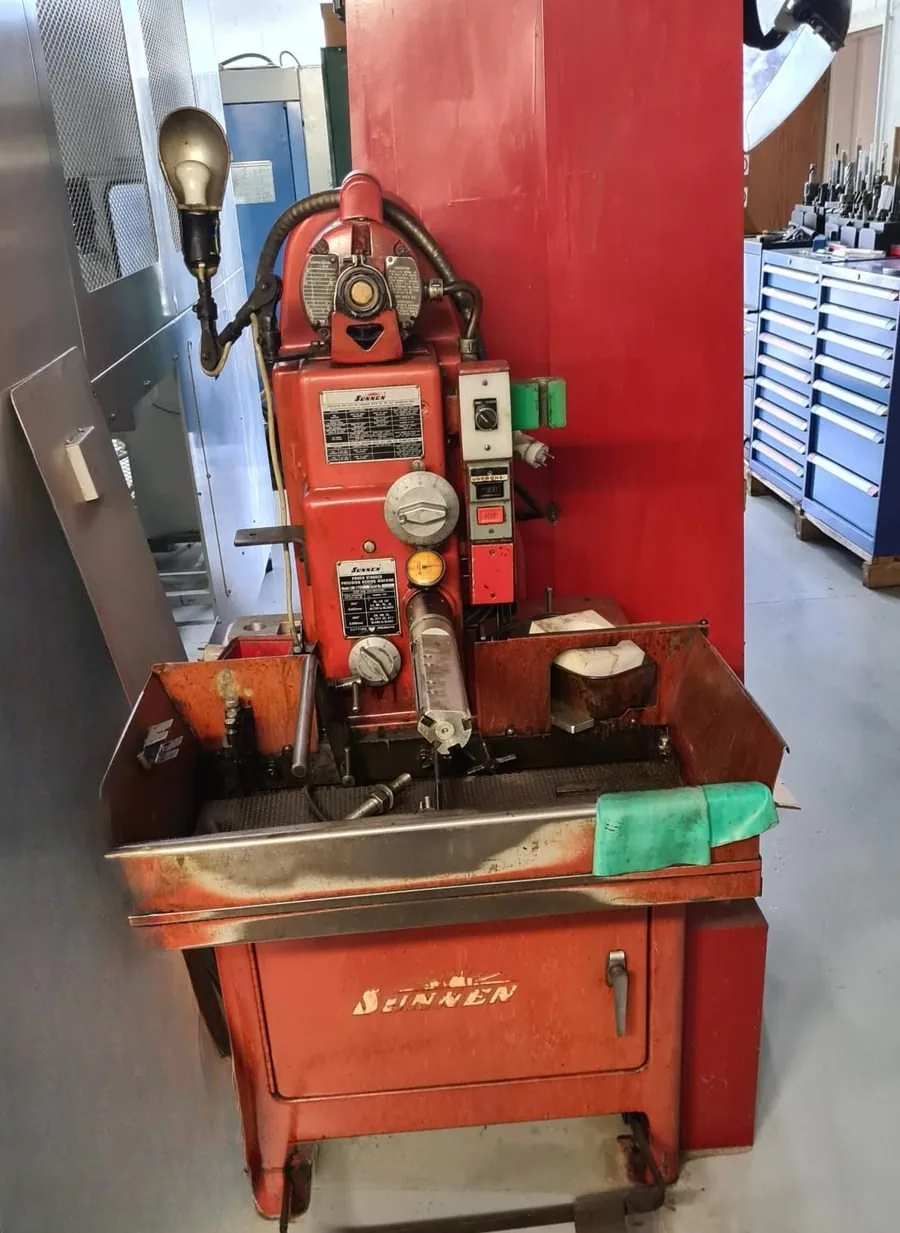
Bores and faces in the same set-up
On our horizontal machining centres, the rotary table presents each face of the part to the spindle without unclamping it. Bores on several faces are machined in the same datum: their relative position does not depend on a second set-up.
In turning, the outer profile, grooves and bore come out of the same set-up; on the SQT 200 MSY, the sub-spindle machines the second face in the same cycle.
Typical parts
- Bushes, bearings and guides.
- Bearing seats and sealing bores.
- Valve plugs and sealed fits.
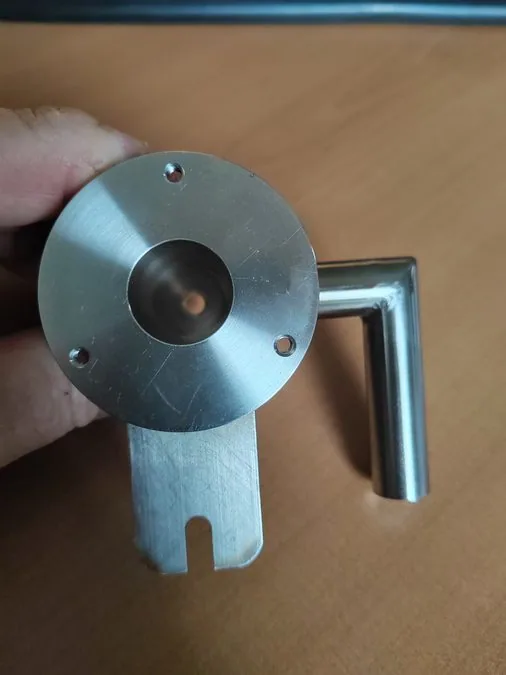
- Nozzles and medical parts in 316L stainless steel.
- Change parts with sealing seats for packaging lines.
Real case: a medical injection nozzle
Class IIb device. The tapered bore, the main function of the part, guides and seals the injection flow.
- 316L stainless steel, EN 10204 3.1 certificate, traceable heat.
- MAZAK QT20N CNC lathe and MAZAK HCN 5000 horizontal machining centre.
- IT7, ±0.009 mm on the bore, achieved by turning without rework or grinding; flange flatness 0.05 mm.
- Mirror polishing by a specialist partner: Ra 0.8 µm specified, Ra 0.2 µm achieved.
- 12 parts in a pilot batch, 8 working days including polishing, each part delivered with its inspection report.
A bore has to be proven
- 3D measuring machineThe KEYENCE XM-5000 measures diameters, centre distances and positions from your drawing or STEP file.
- Non-contact inspectionThe Deltronic DH400 profile projector (400 mm screen) checks profiles, radii, angles and grooves.
- Shop-floor gaugesMicrometers, ring and plug gauges, gauge blocks and dial indicators, at the machine, during production.
- Inspection reportOn request, each dimension is photographed where it was measured: measured feature, nominal value, tolerance, measured value and result.
Boring and honing: your questions
What tolerance can you hold on a bore?
IT5–IT6 as standard on functional diameters, without external grinding. State the target tolerance and fit in your request: we tell you at the quote stage how we will hold them.
What surface finish do you achieve?
Ra ≤ 0.4 µm depending on the geometry by direct machining, down to Ra 0.2 µm on a polished bore.
What diameters and lengths can you hone?
State the diameter, the bore length and the material in your request: we confirm feasibility on our SUNNEN honing machine within 24 hours.
In which materials?
Aluminium (7075, 2017, 5083), 304 and 316L stainless steel, steel, copper, brass, and engineering plastics (HDPE, POM-C, PA6, PEEK). EN 10204 3.1 material certificates on request.
Send your drawing
Drawing, photo or simple description: quote within 24 hours, or 48 hours when we supply the material.
77820 Le Châtelet-en-Brie, France
Upload your specifications
Share your drawings and requirements — detailed quote within 24 hours, or 48 hours when we supply the material.